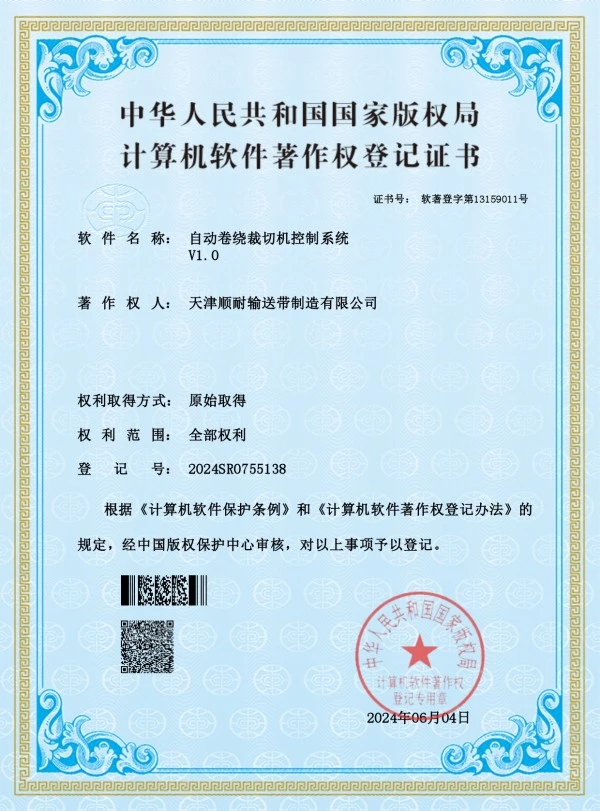
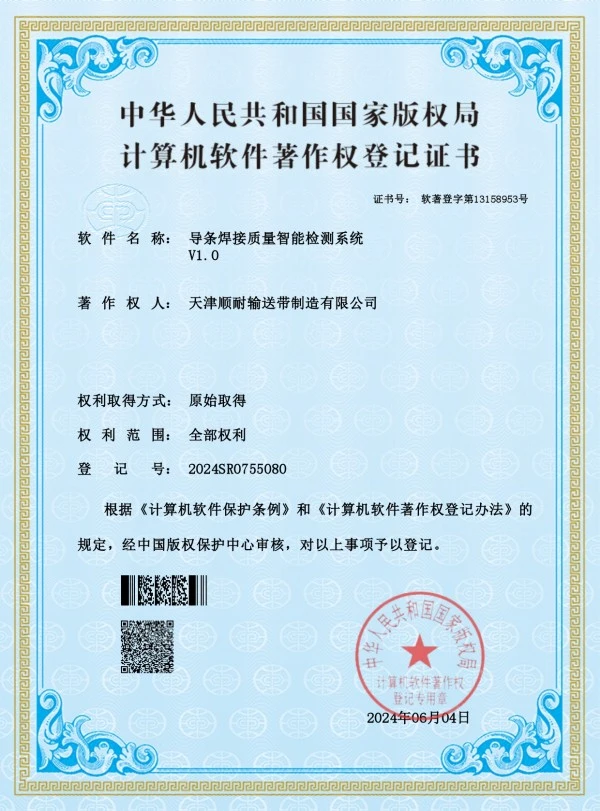
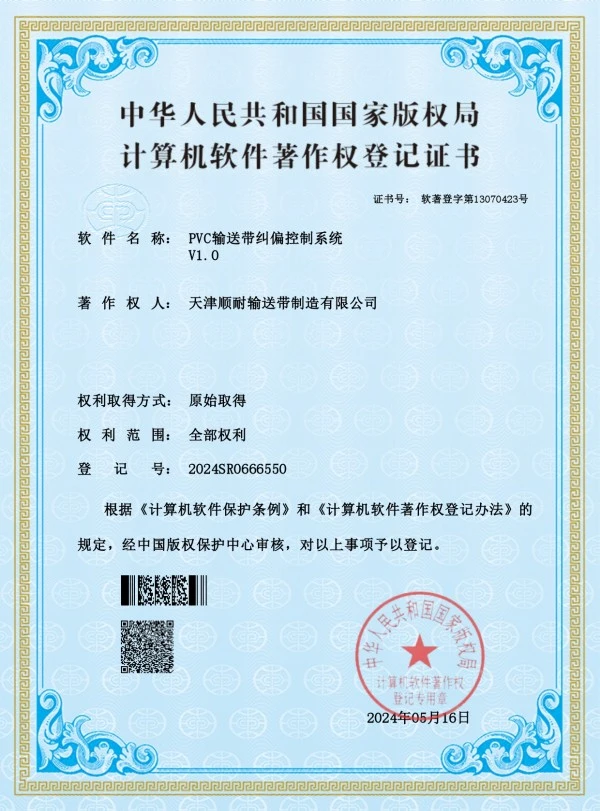
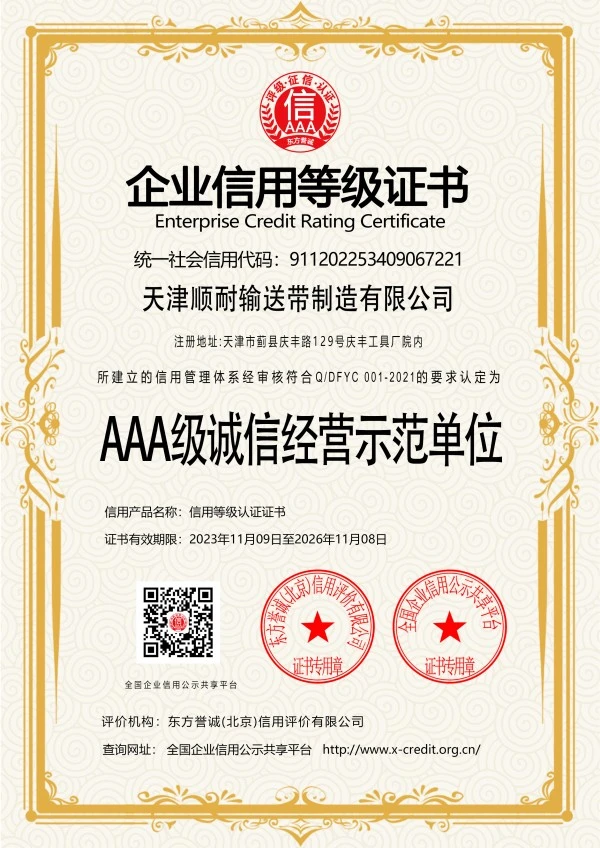
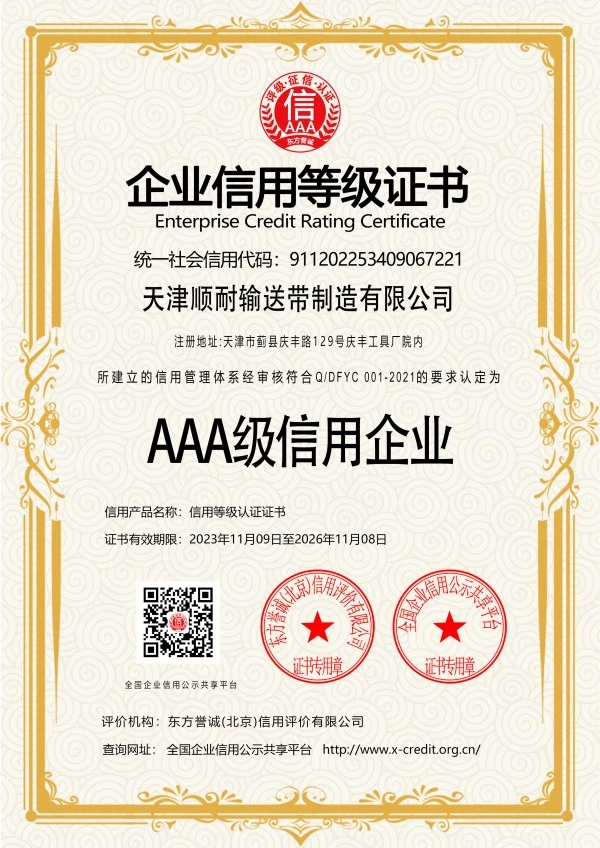
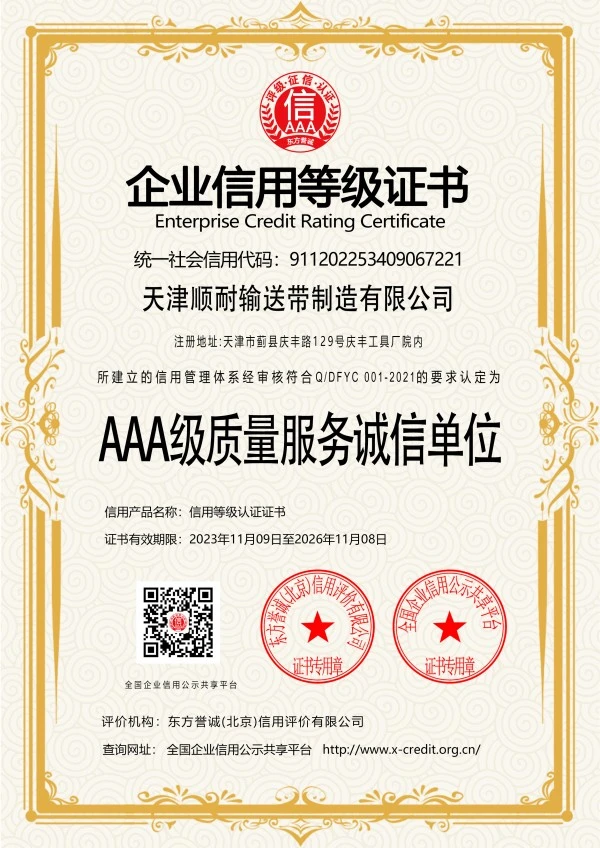
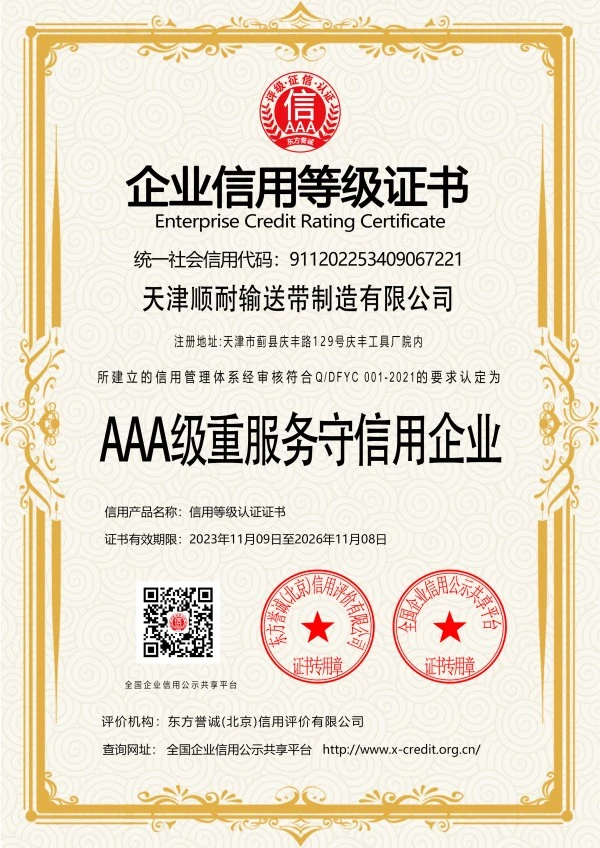
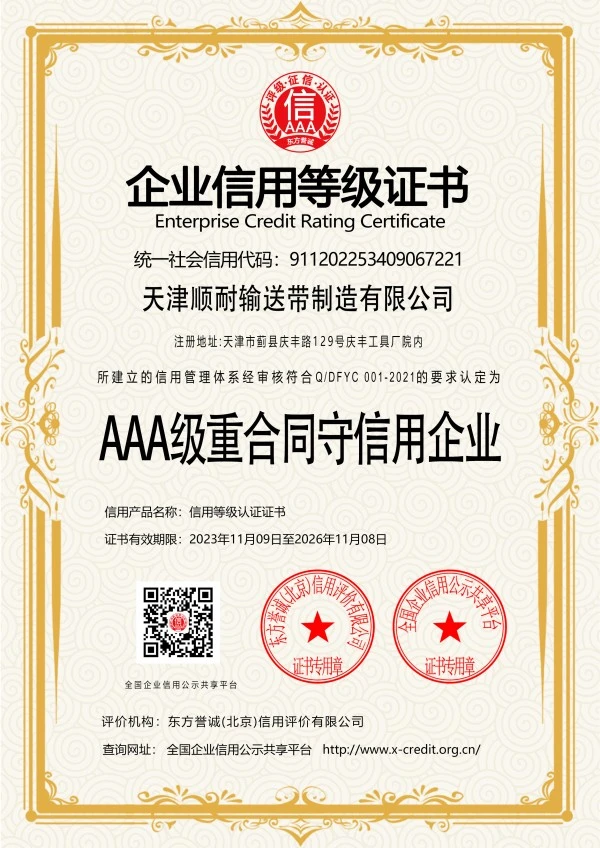
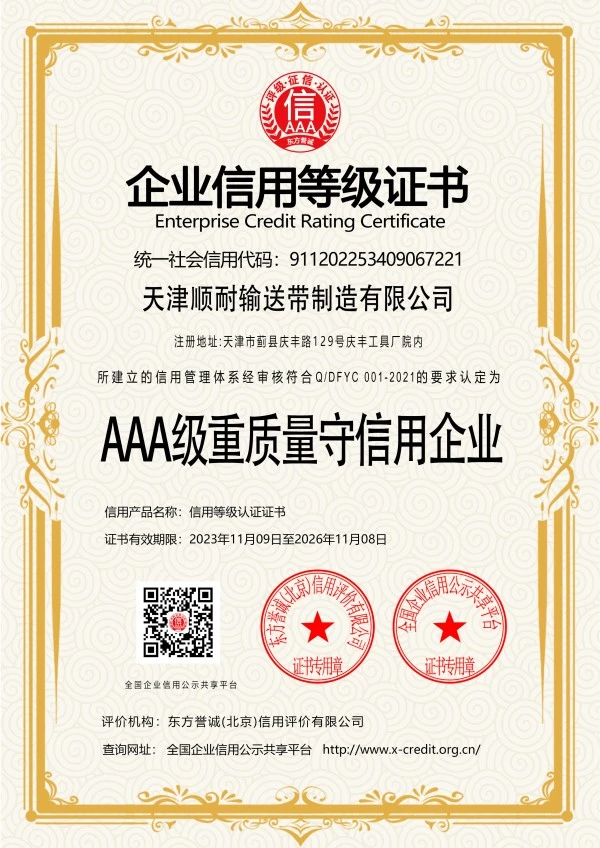
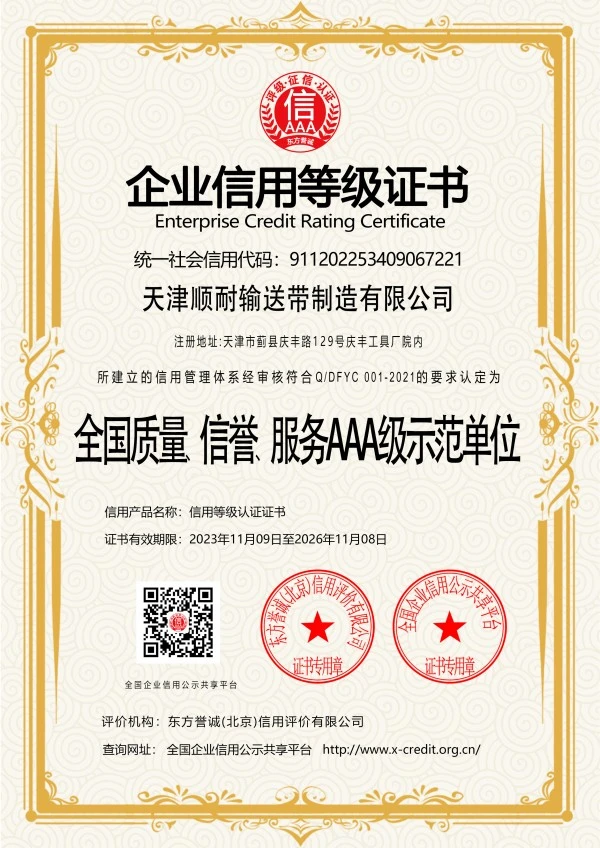
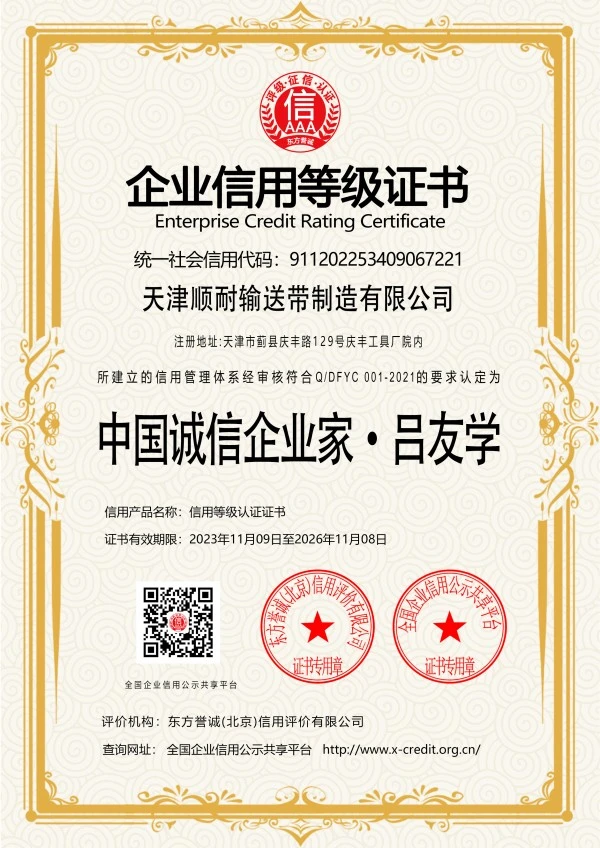
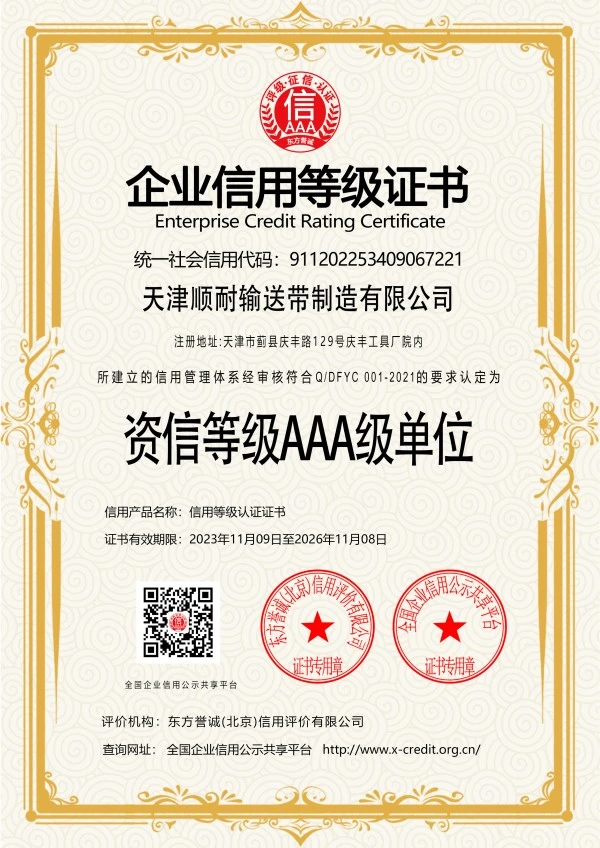
Certificate
1. Superior Quality
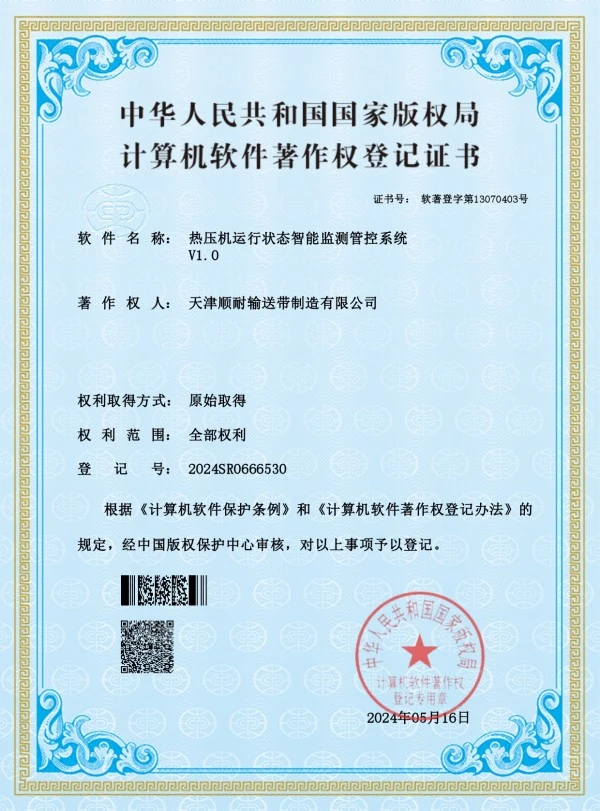
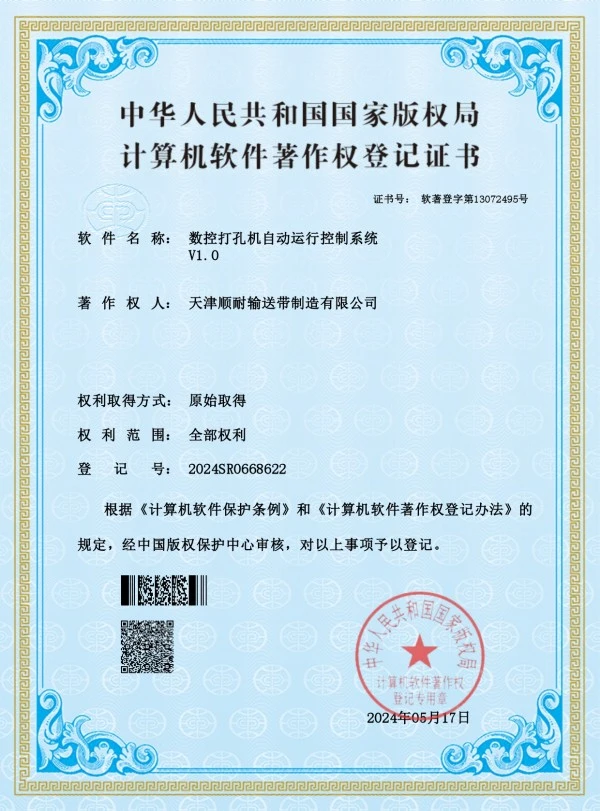
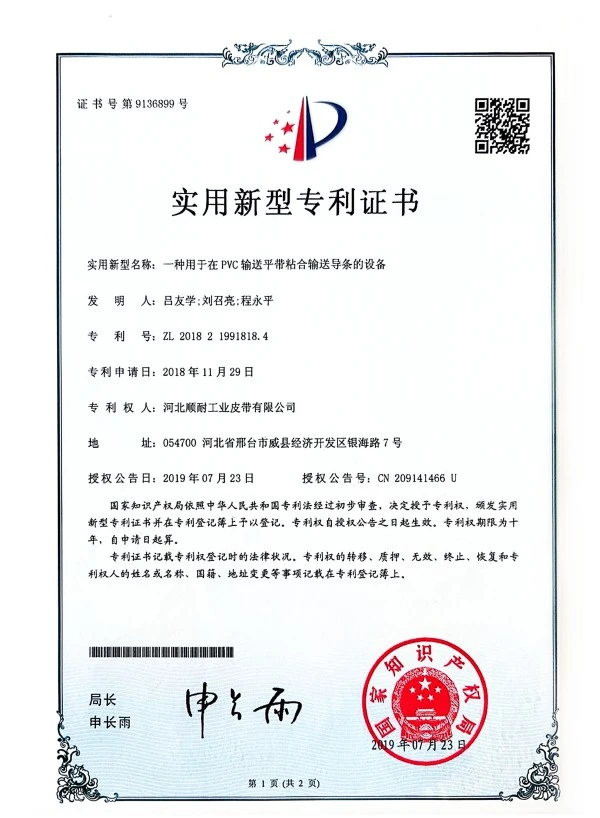
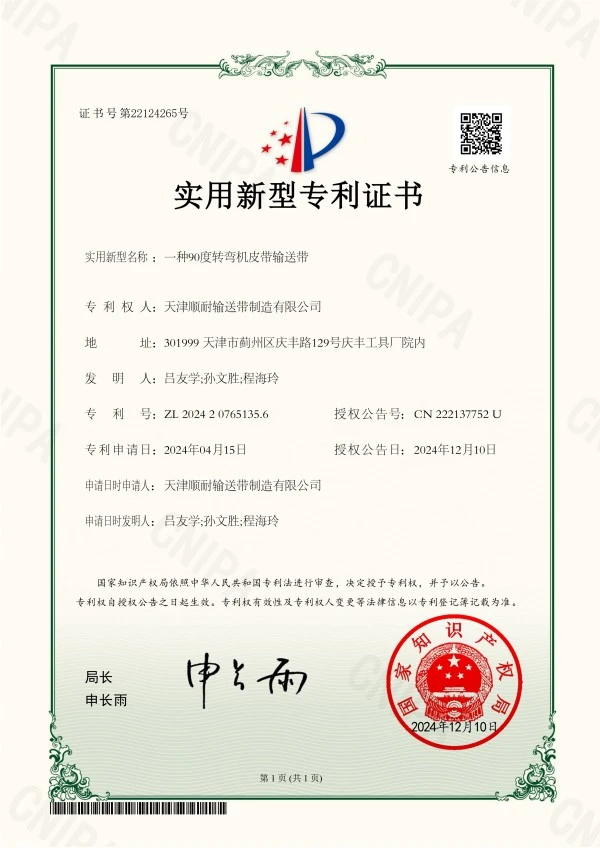
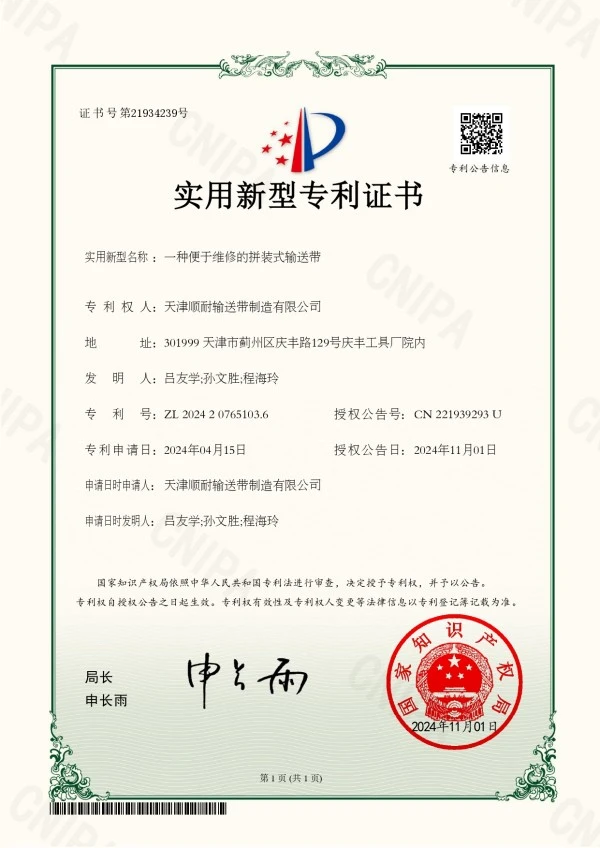
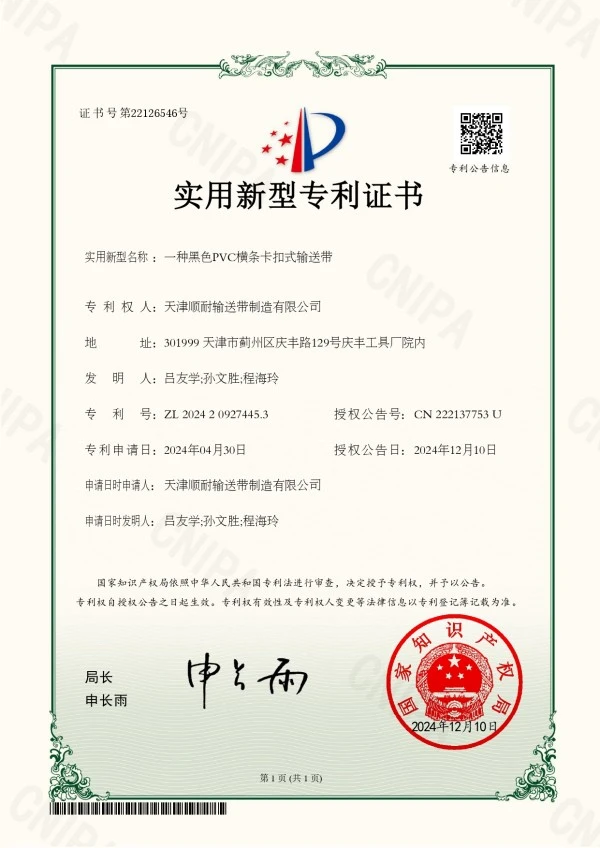
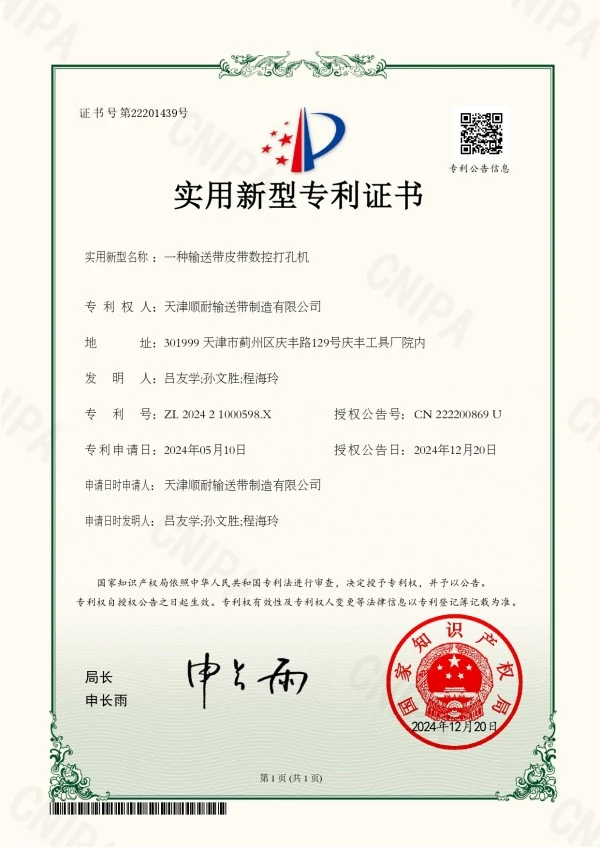
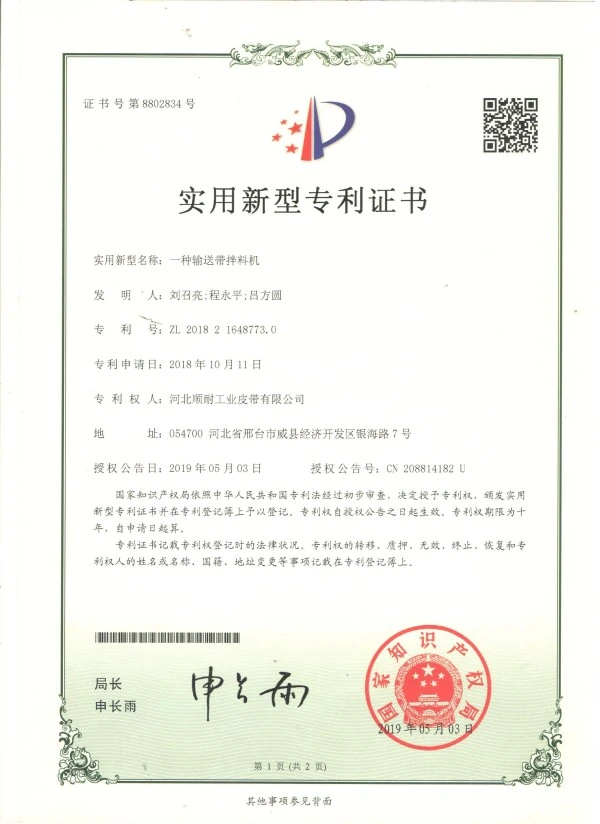
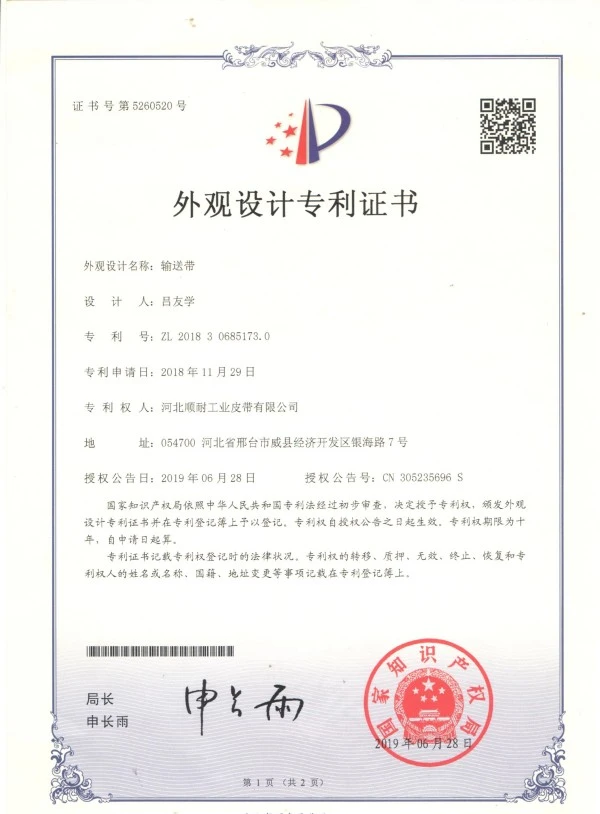
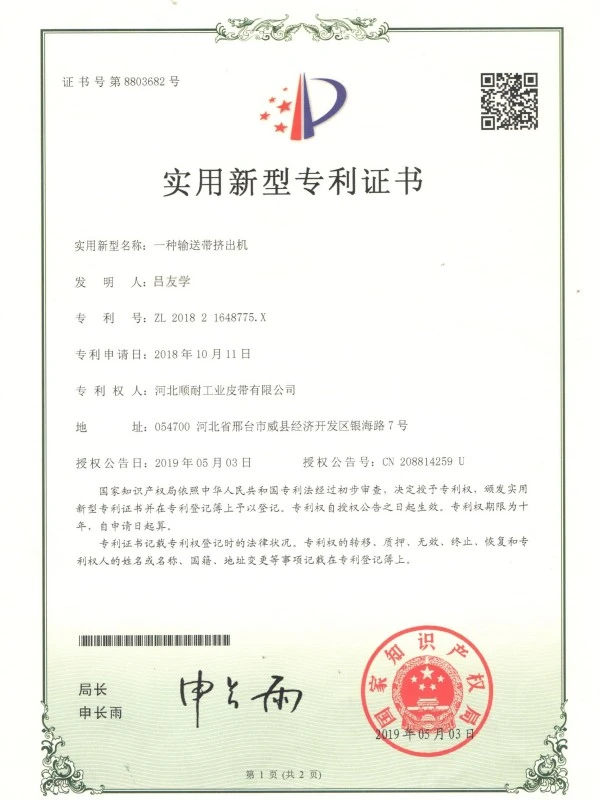
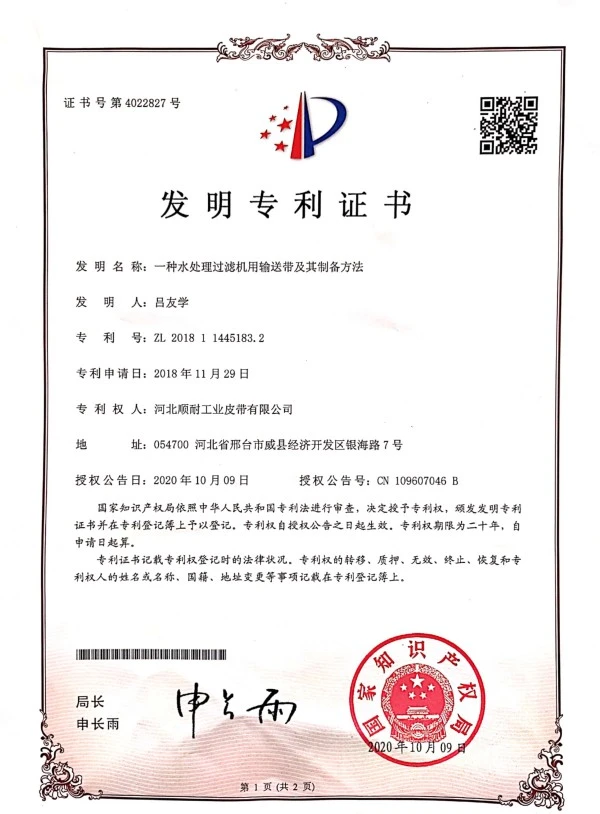
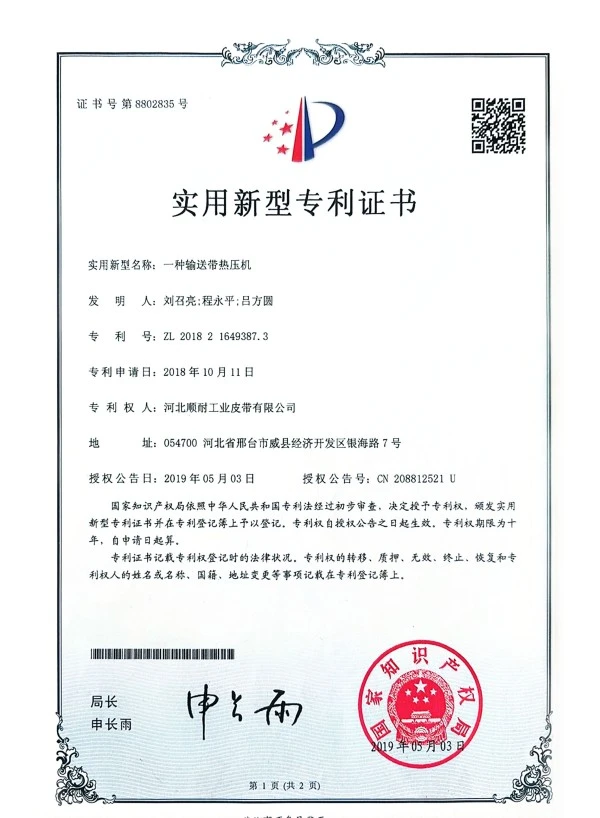
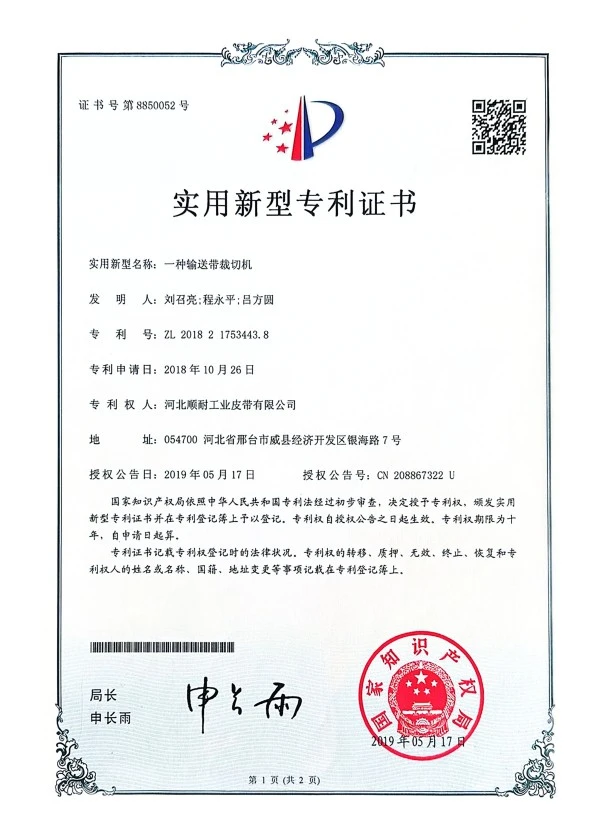
We maintain strict quality control over every stage, from raw material sourcing to production and inspection. By using high-quality raw materials and advanced manufacturing processes, we ensure that every product meets national standards and customer requirements. Our conveyor belts, conveying equipment, and accessories have obtained authoritative certifications such as FDA, MA, and CNAS, along with multiple invention patents. Driven by technological innovation, we continuously introduce advanced R&D equipment and top-tier technical talent, dedicating ourselves to the development and application of new technologies.
2. Professional Service
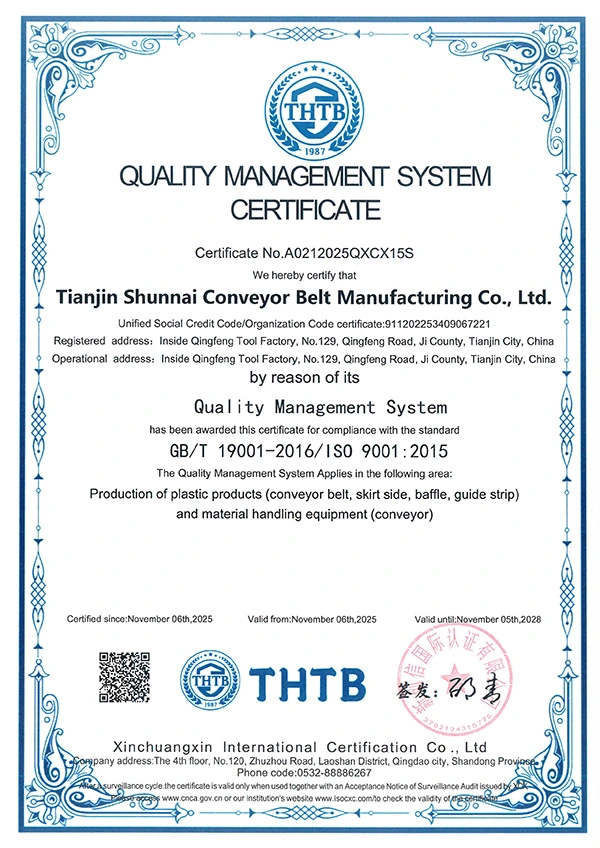
Certified with ISO 9001, our professional R&D team gains deep insights into customer needs, keeps pace with industry trends, and consistently delivers innovative, efficient, safe, and environmentally friendly conveying solutions. In addition, we have established a comprehensive after-sales service system that provides full support throughout the pre-sales, in-sales, and post-sales stages, ensuring a seamless and high-quality experience for our customers.
3. Strong Technical Expertise
With integrated capabilities in design, manufacturing, installation, and maintenance, we have built a strong reputation in the industry. Leveraging our deep technical expertise and rigorous quality control, we ensure fast delivery times and a collaborative, responsive approach, earning the deep trust and broad recognition of our customers.
News Recommendations