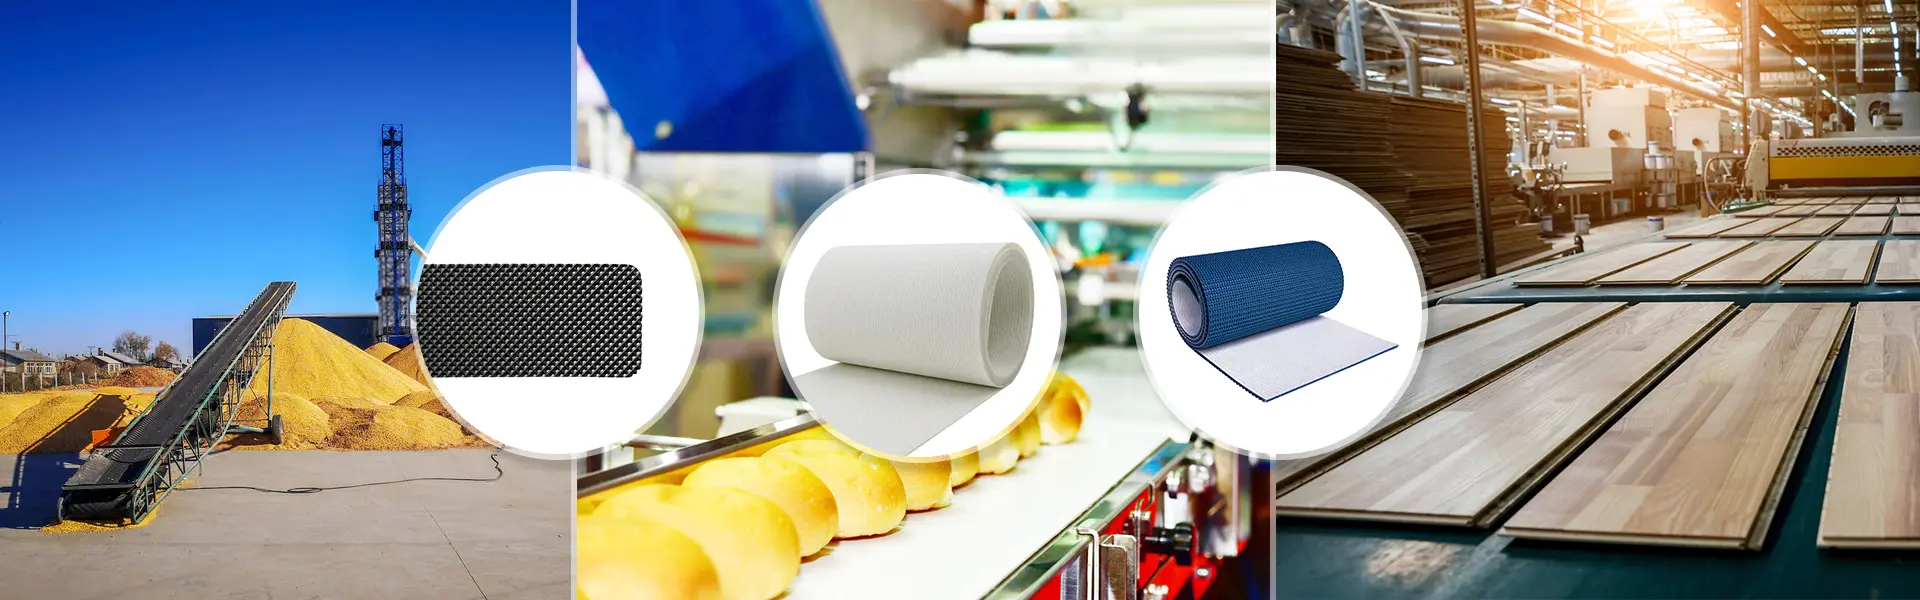
Factory Direct Belt Conveyor for Efficient Bulk Material Handling
Tianjin Shunnai Conveyor Belt Manufacturing Co., Ltd., headquartered in Tianjin, China, is a professional manufacturer and global supplier of industrial conveying equipment. With our own factory covering more than 10,000 square meters, equipped with automated conveyor belt production lines and advanced machining facilities, we specialize in the design, manufacturing, and customization of reliable belt conveyor systems.
As an experienced conveying equipment manufacturer in China, we provide complete solutions for material handling applications across food processing, logistics, mining, packaging, electronics, chemical, and other industries. Through professional engineering capability, strict quality control, and flexible customization services, Shunnai helps customers improve production efficiency and optimize conveying processes.
What Is a Belt Conveyor?
A belt conveyor is a continuous conveying system that uses a belt as the carrying and transporting medium to move materials from one point to another. Driven by motors, pulleys, and rollers, it enables stable and efficient material transportation for both unit loads and bulk materials.
Compared with other conveying equipment, belt conveyors feature simple structure, smooth operation, low maintenance requirements, and flexible installation options. They can be designed according to different material characteristics, conveying distances, production speeds, and working environments.
From lightweight product handling to heavy-duty bulk transportation, belt conveyor systems are widely used as an essential part of modern automated production lines.
Main Conveyor Types
Flat Belt Conveyor
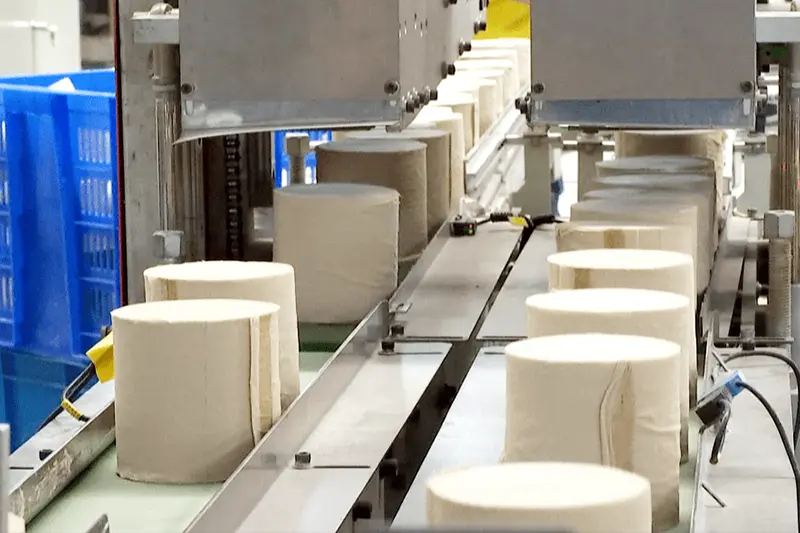
Flat belt conveyors feature a smooth horizontal conveying surface and are widely used for transporting packaged goods, electronic components, food products, and pharmaceutical products.
They provide stable operation, low noise, and easy maintenance. Frame materials such as stainless steel, carbon steel, and aluminum profiles can be selected according to application requirements.
Troughed Belt Conveyor
Troughed belt conveyors use angled idlers to form a U-shaped or V-shaped carrying surface, improving material retention during transportation.
They are commonly used for bulk materials including coal, ore, sand, gravel, grain, and fertilizer. The trough structure helps reduce material spillage and improves conveying capacity.
Cleated Belt Conveyor
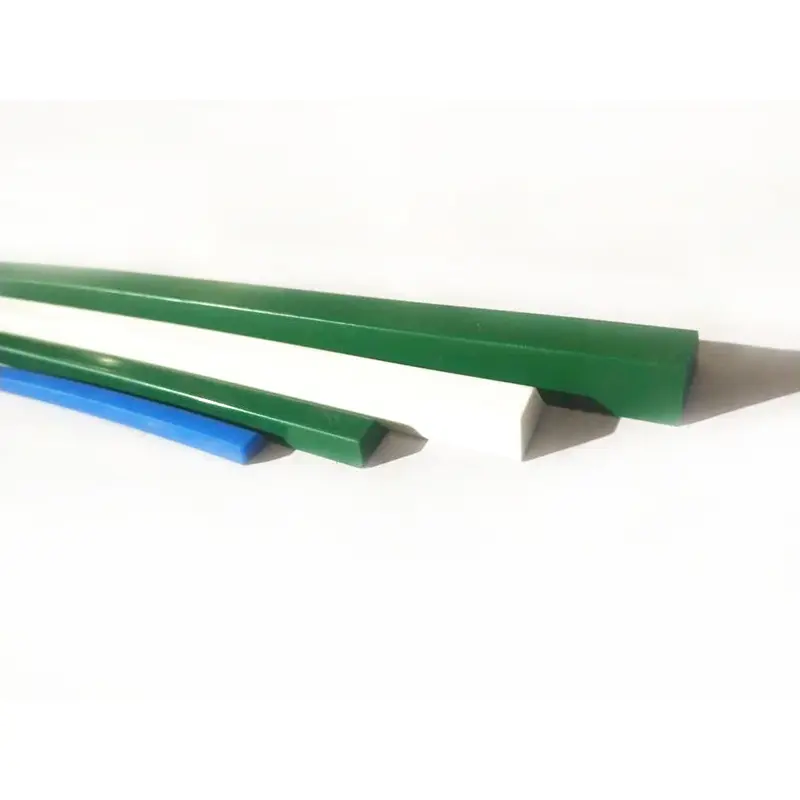
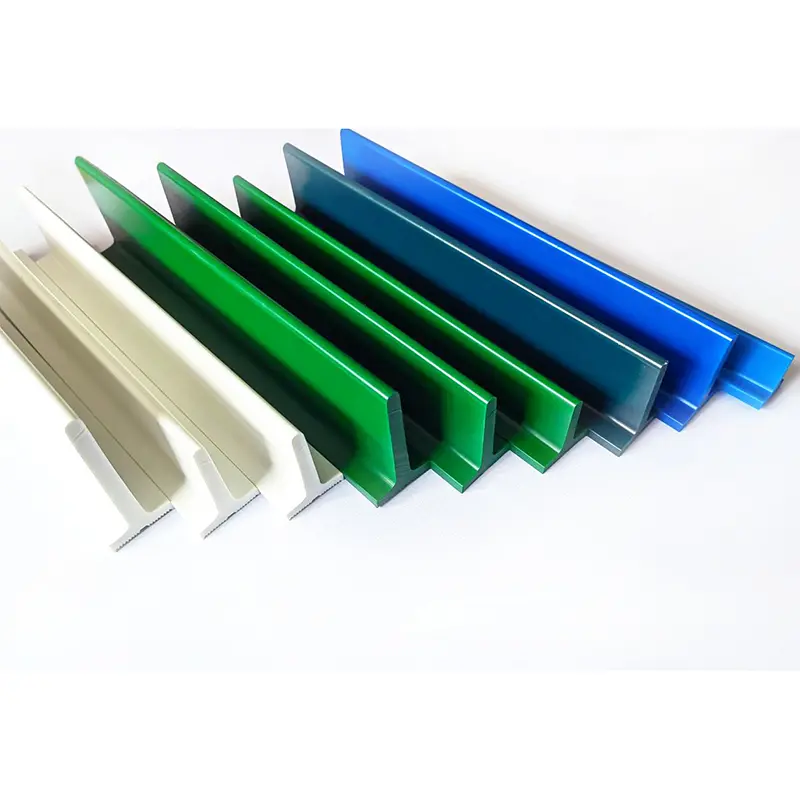
Cleated belt conveyors are equipped with transverse cleats on the belt surface to prevent materials from sliding during inclined conveying.
Combined with sidewalls, they can achieve high-angle conveying for granular, powder, and bulk materials, making them suitable for steep-angle transportation applications.
Mobile Belt Conveyor
Mobile belt conveyors are designed with wheels or movable structures, allowing flexible relocation between different working areas.
They are widely used in warehouses, construction sites, loading areas, and temporary material handling operations where mobility is required.
Food Grade Conveyor
Food grade belt conveyors are manufactured with hygienic designs and food-safe materials such as stainless steel frames and FDA-compliant conveyor belts.
They are suitable for food processing, beverage production, pharmaceutical manufacturing, and other industries requiring easy cleaning and strict hygiene control.
Heavy Duty Conveyor
Heavy duty belt conveyors are designed for large-volume and high-load material transportation.
Using reinforced frames and high-strength conveyor belts, they are commonly applied in mining, metallurgy, ports, power plants, and building material industries where durability and continuous operation are required.
Why Choose Our Conveyor
Flexible Design
Each conveying system can be customized according to product characteristics, factory layout, conveying distance, speed requirements, and automation needs.
Multiple Materials
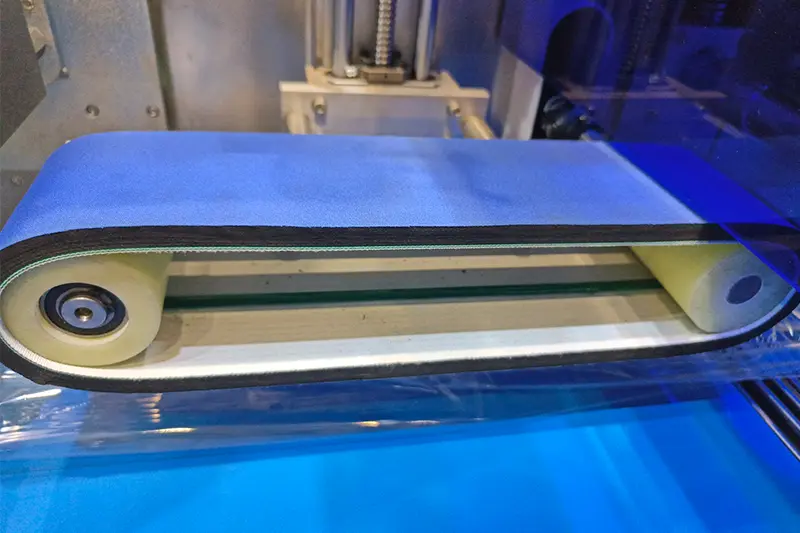
We provide different frame and belt material options, including stainless steel, carbon steel, aluminum profiles, PVC, PU, rubber, silicone, and other specialty materials.
Stable Performance
Strict quality control is applied throughout raw material inspection, production processing, assembly, and final testing to ensure reliable equipment performance.
Complete Service
From initial project consultation and technical design to manufacturing, installation guidance, and after-sales support, we provide complete conveying solutions.
Applications
Food Industry
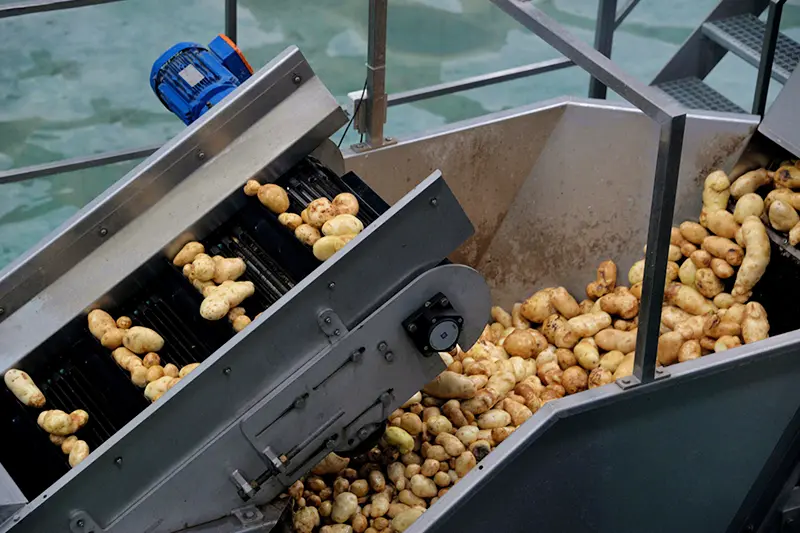
Used for conveying bakery products, meat, seafood, fruits, vegetables, and beverage products.
Food-grade belts provide hygienic operation, easy cleaning, and compliance with food production requirements.
Logistics
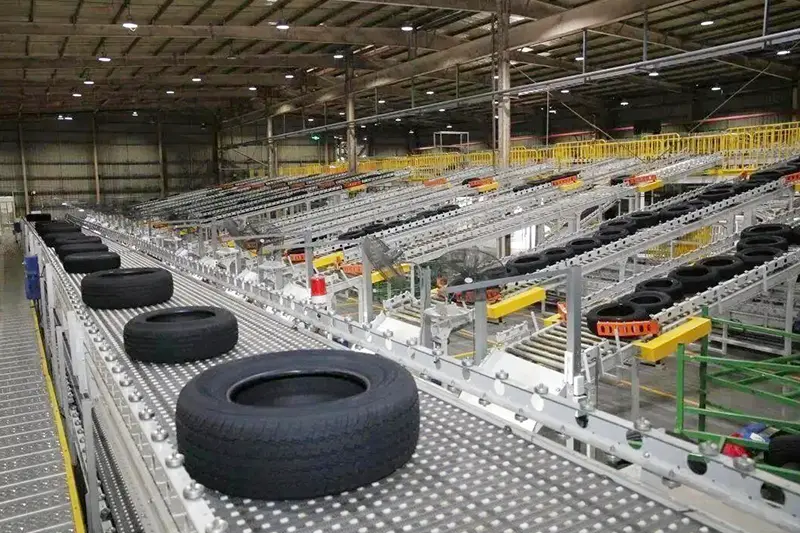
Applied in express sorting, airport baggage handling, warehouse transportation, and distribution centers.
Flat belt conveyors provide smooth and efficient movement of packaged goods.
Mining & Construction
Used for transporting coal, ore, sand, gravel, cement, and other bulk materials.
Troughed and heavy-duty conveyors provide high capacity and long-distance conveying capability.
Electronics Manufacturing
Suitable for assembly lines, inspection systems, and precision production equipment.
Anti-static belts and aluminum frame structures help meet clean and precision manufacturing requirements.
Chemical Industry
Used for transporting powders, granules, and chemical materials.
Special belt materials and corrosion-resistant designs can be selected according to working conditions.
FAQ
How do I select the right conveyor type?
The selection depends on material characteristics, conveying distance, capacity requirements, installation space, and working environment.
Flat belt conveyors are suitable for packaged products, while troughed conveyors are commonly used for bulk materials. Cleated conveyors are recommended for inclined conveying, and heavy-duty models are designed for high-load applications.
What belt materials are available?
Different belt materials are available based on application requirements.
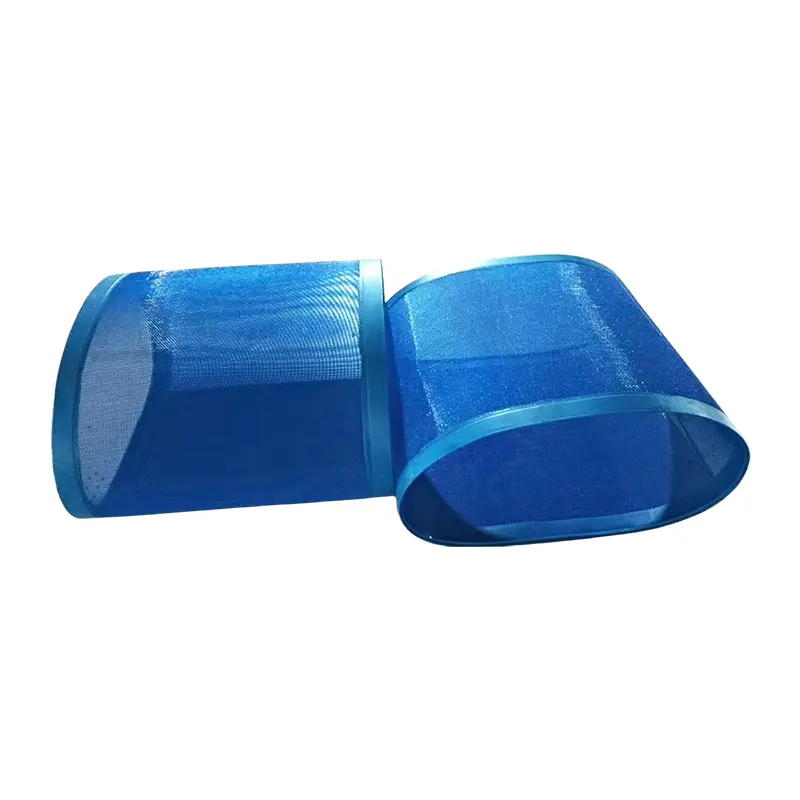
PVC belts are suitable for general industrial conveying, PU belts are preferred for food and hygienic applications, silicone and PTFE belts are used for high-temperature conditions, and rubber belts are commonly applied in heavy-duty environments.
How long can a belt conveyor operate?
The service life depends on belt material, operating conditions, workload, and maintenance.
With proper installation and regular maintenance, industrial belt conveyors can provide many years of reliable operation. Timely inspection of belts, rollers, motors, and drive systems helps extend equipment lifespan.
Can you customize conveyor systems?
Yes. As a professional conveyor manufacturer in China, we provide complete customization services.
We can customize conveyor length, width, height, speed, belt material, frame structure, drive system, and additional functions according to customer production requirements.
Do you provide complete conveying solutions?
Yes. We provide one-stop services including engineering design, equipment manufacturing, customization, installation support, and after-sales service.
Engineering Capability
With years of experience in conveyor equipment manufacturing, Tianjin Shunnai has developed strong engineering capabilities for different material handling challenges. Our technical team understands that every production environment has unique requirements, including product characteristics, factory space limitations, conveying speed, and automation integration.
Beyond standard conveyor solutions, we focus on developing practical systems that match real production conditions. From selecting suitable belt materials and structures to optimizing conveying layouts, we help customers build efficient and reliable material handling processes.
Our experience covers a wide range of industries, including food processing, logistics, mining, electronics, packaging, and industrial manufacturing. By combining manufacturing expertise with application knowledge, Shunnai continues to provide professional conveying solutions that support customers' long-term production goals.
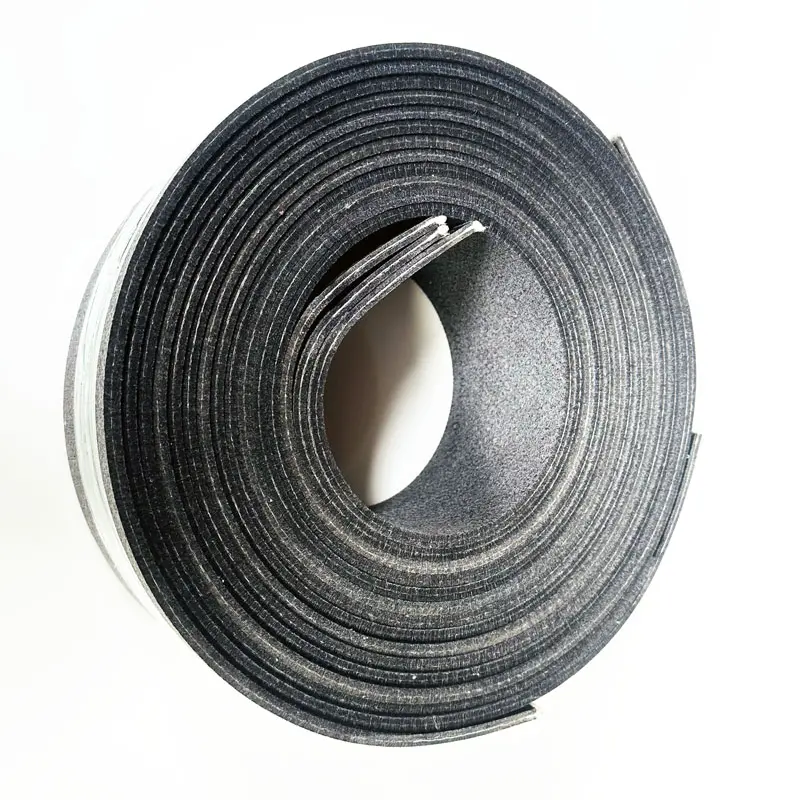
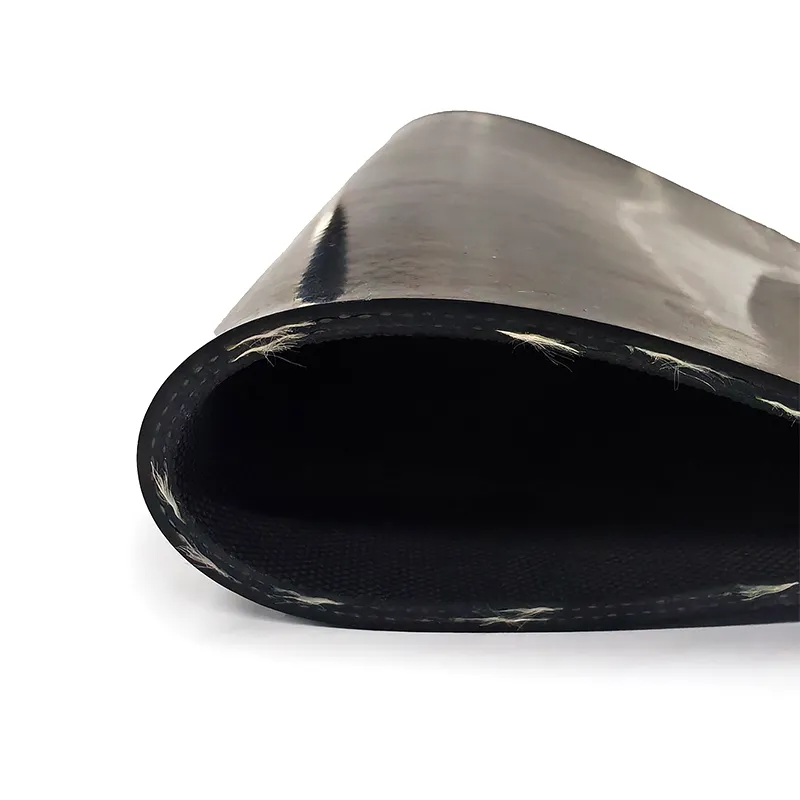
- View as
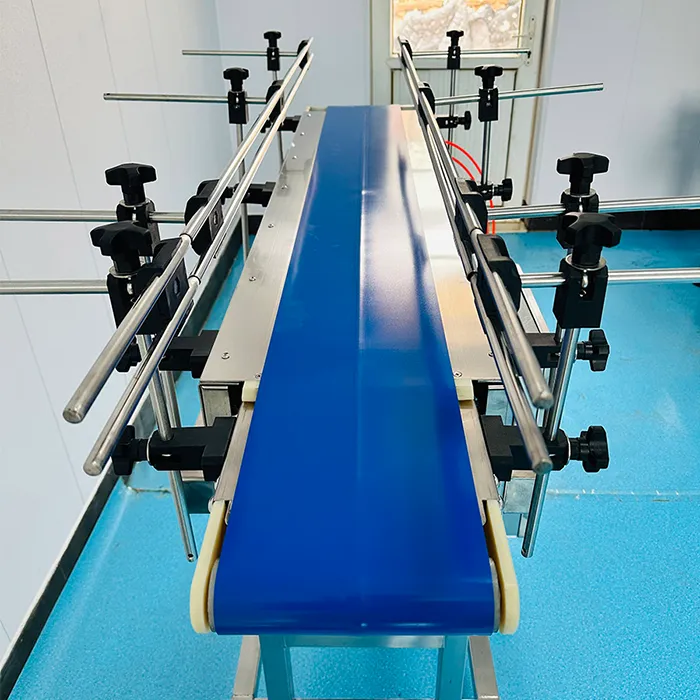
Food-Grade Belt Conveyor
SHUNNAI Food-Grade Belt Conveyor is designed for hygienic material handling in food processing, bakery, meat processing, fruit and vegetable preparation, and packaging production lines. Available with food-grade PU, silicone, PTFE, or PVC belts and optional 304 stainless steel structural components, it can be configured for different product characteristics, operating temperatures, moisture levels, and cleaning requirements.
Whole Machine Food-Grade, No Dead Corners, Easy to Clean
Suitable for Dry, Wet, High/Low Temperature and Oily Conditions
Suitable for Dry, Wet, High/Low Temperature and Oily Conditions
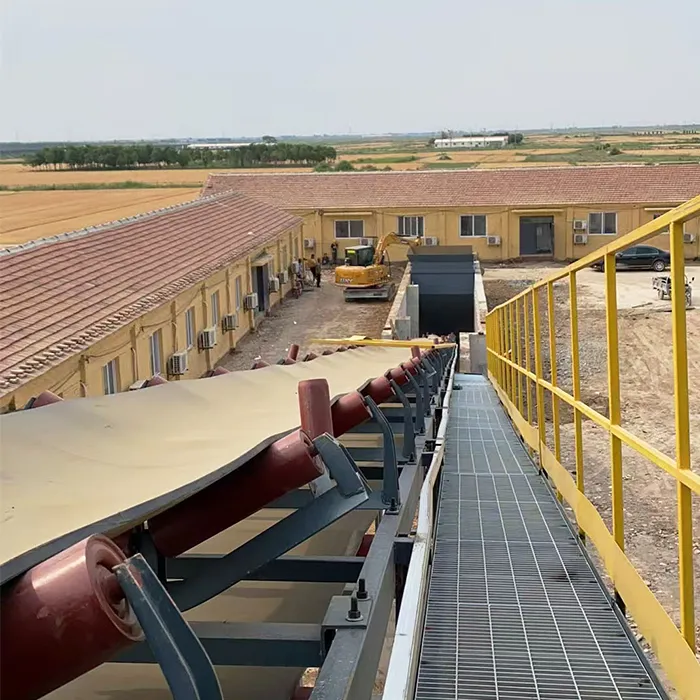
Troughed Belt Conveyor
SHUNNAI Troughed Belt Conveyor is designed for continuous bulk material handling in mining, aggregate production, cement manufacturing, grain processing, biomass energy, and other industrial applications. Its U-shaped belt profile, formed by angled carrying idlers, helps increase the effective loading cross-section and keep loose materials centered during conveying.
U-Shaped Trough Gathers Bulk Materials
High Capacity, Low Spillage
Continuous Transfer for Mining, Grain and Building Materials
High Capacity, Low Spillage
Continuous Transfer for Mining, Grain and Building Materials
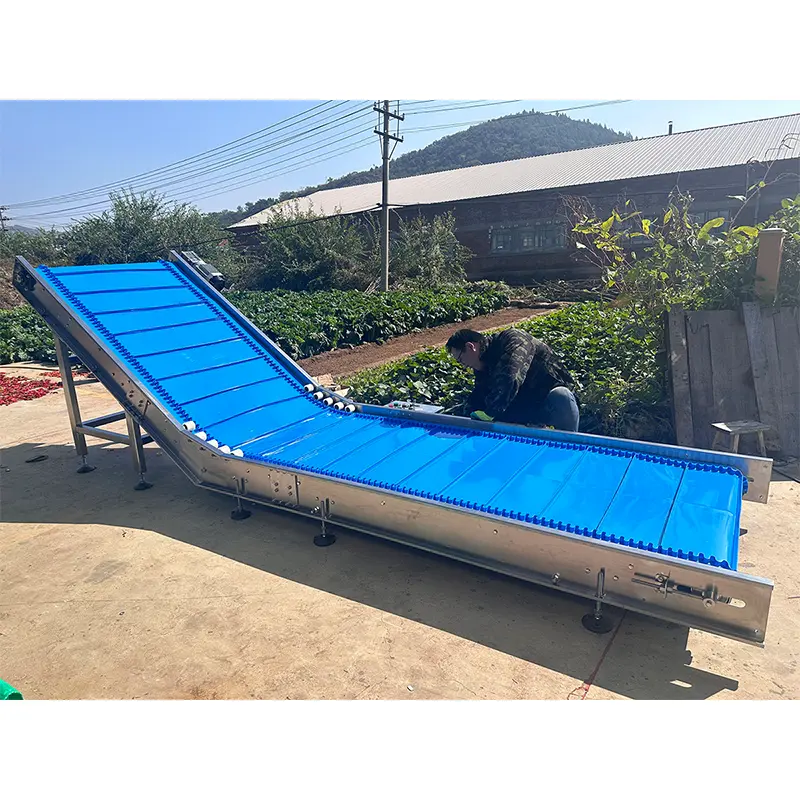
Corrugated Sidewall Belt Conveyor
Corrugated Sidewall Belt Conveyor from SHUNNAI is designed for steep-angle conveying, vertical lifting and space-saving material transfer. With customized sidewalls, cleats and durable belt materials, it provides stable, spill-resistant conveying solutions for food, grain, chemical, mining and industrial applications. Manufactured under ISO 9001:2015 quality management system with professional testing support.
1.Steep-angle conveying
2.Anti-spillage design
3.Heavy-load stability and customizable
2.Anti-spillage design
3.Heavy-load stability and customizable
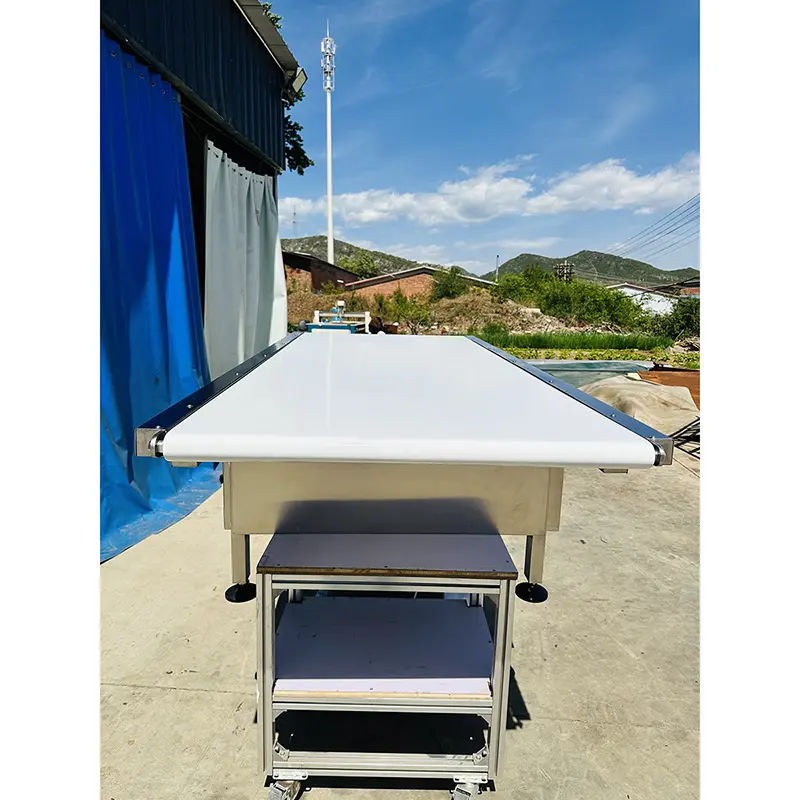
Flat Belt Conveyor
SHUNNAI Flat Belt Conveyor is designed for manufacturers requiring stable, accurate and customized horizontal conveying solutions. With multiple frame options, flexible belt selections and strict quality control based on GB/T 19001-2016 / ISO 9001:2015 standards, SHUNNAI provides reliable conveyor systems for food, pharmaceutical, electronics, packaging and industrial applications.
1.Multimaterial customization for all scenarios
2.Easyclean, sanitary grad
3.Ultrasmooth operation
2.Easyclean, sanitary grad
3.Ultrasmooth operation
SHUNNAI is a professional Belt Conveyor manufacturer and supplier in China. We have an experienced sales team, professional technicians, and an after-sales service team.
News Recommendations